Thirty years in precision metrology, brought straight to the floor: the program gets written, proven out, and signed off against the actual part, not a model of it.
CMM (coordinate measuring machine) programming, troubleshooting, coverage, FAI support, and training, plus offline program builds when the machine can't stop measuring. Most of it happens the old-fashioned way: standing at the machine, where fixture quirks, surface finish, and print oddities actually show up.
New programs are written and proven out on the CMM, against actual parts and fixturing: start to finish, in one visit.
Programs and data come together to get an FAI through review without tying up the quality manager or shop personnel to figure it out.
An inherited program that's slow, unstable, or just wrong gets diagnosed and fixed on the machine, in the actual production environment.
Programs get drafted ahead of first parts arriving, then finalized and signed off in person once the part's in hand.
An experienced contract programmer on your floor when the need arises: departures, leave, backlogs
Custom training at your machine with your parts, your prints, your probing, and the software version you actually run. Billed by the hour, not the seat.
The fixture doesn't sit right, the surface finish throws the probe off, or the print doesn't quite match the part.
Better to find that out standing next to the machine than over email. One visit: program written, proven out, and signed off; no back-and-forth waiting on a file that "should" work.
Based in the Indianapolis area, available to travel nationwide
Daily rate available: click here for full pricing details
Tim Hogan's path into CMM work started in a manufacturer's quality lab in the mid-1990s at Dynamic Corporation: reading blueprints, learning GD&T, and measuring parts by hand with calipers, micrometers, optical comparators, and height and radius gauges before ever touching a CMM. That manual foundation still shapes how a print gets read today, not just how a program gets written.
CMM programming came next, then responsibility for it. At Gibbs Die Casting, that meant writing programs for incoming work and eventually managing a department running eight CMMs across layout and quality control. Back at Dynamic's Holland, Michigan lab, it meant running a seven-CMM operation with a vision system, plus a steady stream of contract assignments at other companies: program management, quality lab consulting, on-site programming, the kind of work that means walking into an unfamiliar shop and an unfamiliar fixture and getting a working program out the other side.
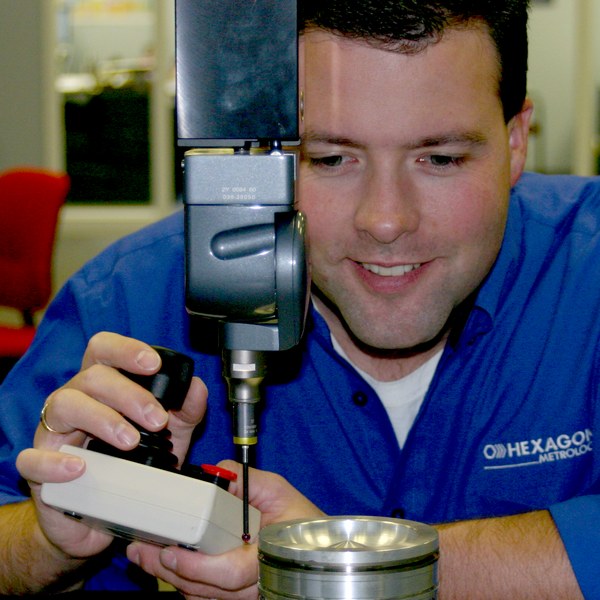
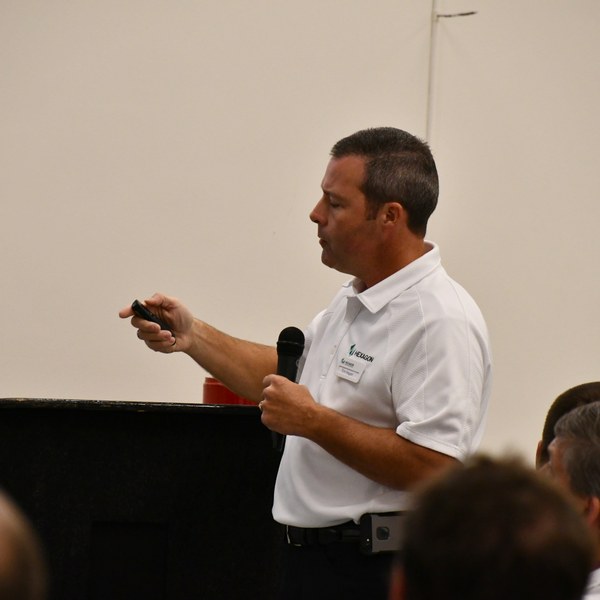
The Hexagon years put all of it to work at scale: teaching classroom PC-DMIS training courses, delivering on-site CMM training and applications support directly on customers' machines, and continuing contract inspection work in between. Close to three decades of metrology in total, solving one challenge after another and making sure the program ran, the accuracy was right, and the customer was not just satisfied, but happy. That range of experience is what's back on the floor, your floor, doing the programming once again.
Send over the part, the print, and roughly when someone's needed on the floor. A follow-up comes back with timing and a straightforward quote.